Drying Endpoint Detection: Gravimetric Method and Its Alternatives
A vacuum oven is a combination of a vacuum system, a heating system and a pressure vessel, and each of those has its own failure modes. Understanding which one is limiting your process turns a maintenance problem into a specification problem.
A vacuum oven is a combination of a vacuum system, a heating system and a pressure vessel, and each of those has its own failure modes. Understanding which one is limiting your process turns a maintenance problem into a specification problem.
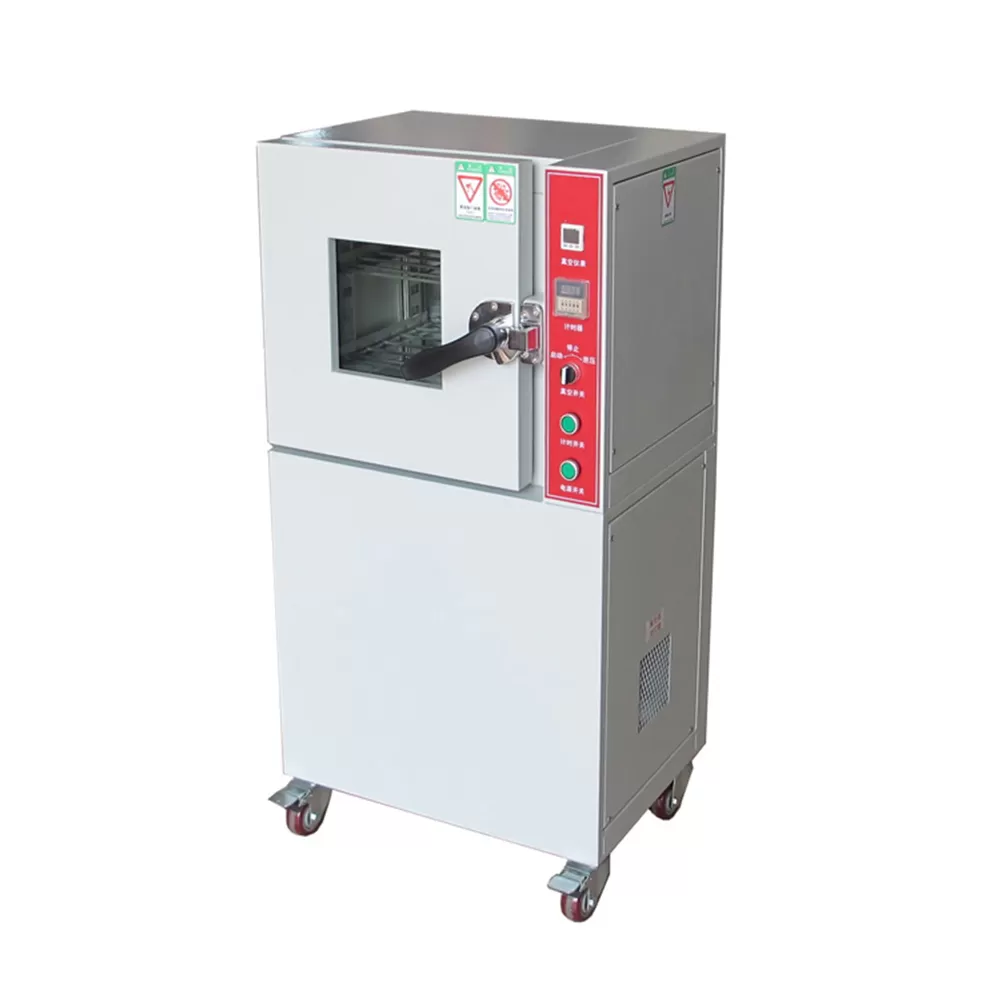
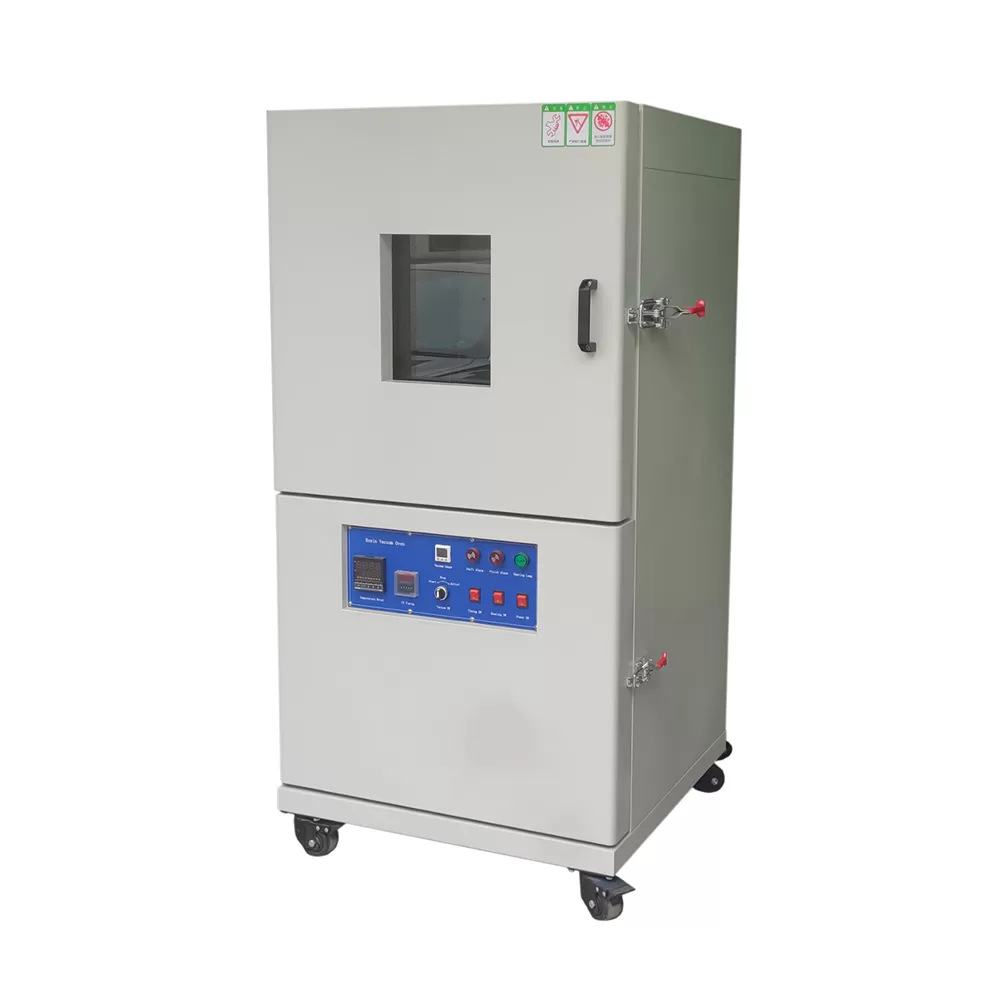
Applying that to a real purchase is easier when the equipment comes from a supplier that builds rather than assembles. 27L Vacuum Oven is a typical example of a machine where the specification sheet is only half the story, because the fabrication and commissioning route determines how the numbers behave in service.
What to verify before you specify
1. Know the working pressure you actually need
Different processes need different vacuum levels, and demanding a deeper vacuum than the process requires costs energy and increases pump wear for no benefit.
2. Pump type determines the achievable level
A rotary vane pump reaches a practical floor around the single-digit mbar range; reaching deeper requires a diffusion or turbo stage. The specification should match the process, not exceed it.
3. Backstreaming and contamination control the result
A pump that backstreams oil vapour into the chamber will contaminate the product. Traps and proper pump placement are part of the system, and the chamber door seal has to be considered too.
4. Chamber material and heating method affect the profile
A stainless inner chamber with external heating avoids condensation on the walls, and uniform heat transfer depends on the heating arrangement rather than the heater wattage alone.
5. The temperature sensor must sit in the working volume
A sensor mounted on the chamber wall will read differently from the load. For a process with a tight drying specification, the sensor position determines whether the recorded profile is meaningful.
6. Loading affects drying time
A dense load in a large chamber takes far longer than the same load in a small one, because the chamber has to heat the load as well as the air. Planning for realistic loading is part of the selection.
Mistakes that show up in the acceptance report
- Ordering a much deeper vacuum than the process requires.
- Placing the pump where backstreaming oil can reach the chamber.
- Calibrating against a wall-mounted sensor rather than the working volume.
- Underestimating drying time for a dense or high-moisture load.
Shipping test equipment across an ocean is a manufacturing decision, not a logistics one
The condition a machine is in when it reaches the laboratory was determined when the crate was built.
Crating is a fabrication task, so it belongs in the factory. Frames, corner castings and access panels are restrained against transit forces as part of the production route, not improvised by a packing team on the last afternoon.
A machine that travels in a container can arrive with condensation inside it, so acclimatisation before energising is a procedure the supplier should specify in the documentation set rather than discover on site.
Export crating, anti-rust treatment and the complete document set are prepared in-house, which removes a whole category of delay between the production floor and the receiving dock.
- In-house Manufacturing: Every machine is engineered, welded, assembled and tested under one roof. Two production plants control tolerances from raw sheet steel to final calibration.
- OEM & ODM Engineering: Drawings, PLC logic, instrumentation and chamber geometry are developed in-house, so non-standard chamber sizes and test profiles ship without external dependencies.
- Full In-House Calibration: Temperature, humidity, pressure and load cells are calibrated on our own accredited benches before shipment, with certificates issued per unit.
- QC at Every Stage: IQC, IPQC and OQC gates sit between material intake, welding, assembly and dispatch. Nothing leaves the line without a signed inspection record.
How the equipment is produced
The production route below is the one every HAOEN machine follows. It is listed because the steps a manufacturer controls are the steps that determine whether your laboratory receives a machine that performs as specified on the day it is commissioned, and still performs two years later.
- Engineering Drawing — Chamber geometry, load frame, airflow and instrumentation are modelled and reviewed before any steel is cut.
- Material Intake — Sheet metal, compressors, sensors and electrical parts pass incoming inspection against incoming QC checkpoints.
- Cutting & Bending — CNC cutting and press braking form the chamber body, liner and door frame to millimetre drawings.
- Welding & Forming — TIG and robot welding seal the chamber, followed by stress relief and surface treatment.
- Assembly & Wiring — Refrigeration, electrical cabinets, sensors and control panels are installed and wired to the schematic.
- Debugging & Calibration — Commissioning runs temperature, humidity, vibration and load profiles; data is logged per unit.
- Packing & Documents — Crating, manuals, certificates and the QC file are completed and sealed for dispatch.
- Delivery & Support — Shipment tracking, on-site installation and operator training are arranged with local partners.
Equipment referenced in this guide
- 27L Vacuum Oven — Vacuum Oven, manufactured in-house with per-unit calibration.
- Vacuum Oven — Vacuum Oven, manufactured in-house with per-unit calibration.
- 64L Vacuum Oven — Vacuum Oven, manufactured in-house with per-unit calibration.
Conclusion
Specification is where a procurement process starts, but it is not where the result is decided. The variables that separate a repeatable test from an arguable one are the ones the manufacturer controls: the geometry of the chamber, the tightness of the weld, the stability of the control loop and the discipline of the calibration bench. Those are the variables worth asking about, because they are the ones that will still be there when the instrument is three years old and a colleague asks why the new machine and the old one give different numbers on the same specimen.
If you have a specification in front of you that has a profile, a volume and a tolerance, send it over. Our engineers will respond with a configuration, a lead time and the specific items in the manufacturing route that will affect your result.