Why Light-Cooling Systems Decide UV Aging Test Chamber Performance
A UV aging chamber is defined first by its light source, and second by how well it controls the heat that light source generates. Buyers who focus on lamp wattage alone often end up with a chamber that cannot hold the prescribed black-panel temperature.
A UV aging chamber is defined first by its light source, and second by how well it controls the heat that light source generates. Buyers who focus on lamp wattage alone often end up with a chamber that cannot hold the prescribed black-panel temperature.
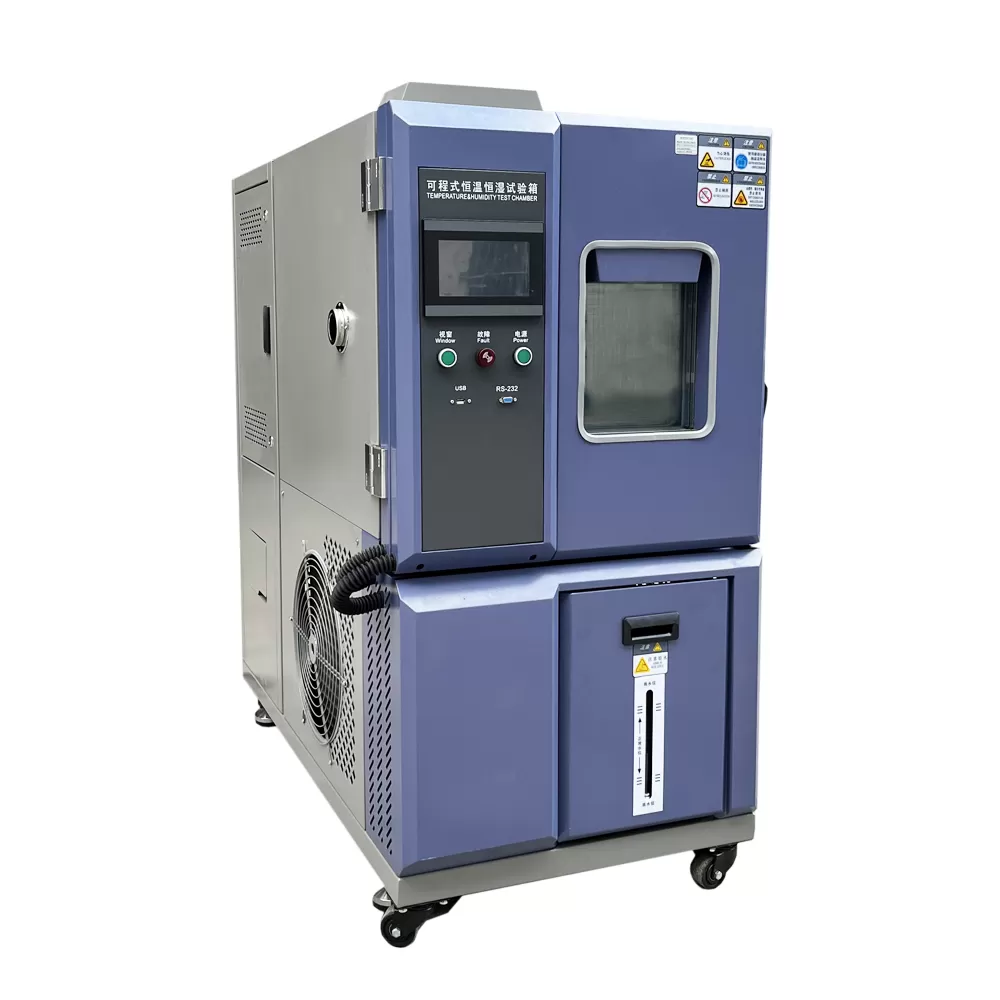
Applying that to a real purchase is easier when the equipment comes from a supplier that builds rather than assembles. 150L Climate Test Chamber is a typical example of a machine where the specification sheet is only half the story, because the fabrication and commissioning route determines how the numbers behave in service.
What to verify before you specify
1. Lamp choice determines the spectrum
UVA-340 simulates sunlight above 300 nm, UVA-351 simulates sunlight through window glass, and UVB-313 is an accelerated version with a higher short-wave output. Xenon arc provides a fuller spectrum including visible light. The choice is dictated by the material and the standard.
2. Irradiance control and uniformity
The chamber must hold a specified irradiance in W/m² across the sample plane, and the sensor has to see the same value that the reference instrument would. Lamp ageing shifts output, so the control loop and the calibration schedule matter as much as the initial setting.
3. Black panel temperature is the hard number
The sample surface temperature is controlled through a black panel sensor, not through chamber air. A chamber with strong cooling can hold air temperature but still fail on black panel, because the cooling air is passing over the sensors.
4. Condensation control for water-spray cycles
Many UV aging standards include a water spray or condensation phase. The spray has to reach the sample uniformly and the chamber must not suffer from condensation pooling in the base.
5. Sample rotation for uniform exposure
Intermittent exposure requires the sample to move between the lamp and the shaded position. The rotation mechanism needs to be repeatable and the cycle count must be logged.
6. Lamp replacement and recalibration
UV lamps have a finite life and their output changes noticeably before they fail. Plan the replacement interval and the recalibration that follows it into your maintenance plan.
Mistakes that show up in the acceptance report
- Specifying lamp type by price rather than by the standard the customer requires.
- Assuming chamber air temperature equals sample surface temperature.
- Forgetting lamp replacement and the recalibration that has to follow it.
- Running a water-spray phase in a chamber without a proper spray ring or drainage.
Why the manufacturing route changes your results
Test equipment is usually specified as a specification sheet, but the route the machine took to get to you is embedded in the numbers it will produce.
Chamber geometry, liner material and insulation thickness are decided at the design stage and fixed at fabrication. A chamber whose frame was welded on a jig has a different thermal behaviour from one assembled from folded sheet, and the difference shows up as the uniformity figure.
Refrigeration selection, sensor placement and control loop tuning are done in-house. When a compressor, a controller and a chamber are specified by three different suppliers, the integration is nobody’s responsibility and the result is drift that nobody diagnosed.
Calibration on our own accredited benches before shipment means the certificate describes the machine you received, not the model it was assembled from.
- In-house Manufacturing: Every machine is engineered, welded, assembled and tested under one roof. Two production plants control tolerances from raw sheet steel to final calibration.
- OEM & ODM Engineering: Drawings, PLC logic, instrumentation and chamber geometry are developed in-house, so non-standard chamber sizes and test profiles ship without external dependencies.
- Full In-House Calibration: Temperature, humidity, pressure and load cells are calibrated on our own accredited benches before shipment, with certificates issued per unit.
- QC at Every Stage: IQC, IPQC and OQC gates sit between material intake, welding, assembly and dispatch. Nothing leaves the line without a signed inspection record.
How the equipment is produced
The production route below is the one every HAOEN machine follows. It is listed because the steps a manufacturer controls are the steps that determine whether your laboratory receives a machine that performs as specified on the day it is commissioned, and still performs two years later.
- Engineering Drawing — Chamber geometry, load frame, airflow and instrumentation are modelled and reviewed before any steel is cut.
- Material Intake — Sheet metal, compressors, sensors and electrical parts pass incoming inspection against incoming QC checkpoints.
- Cutting & Bending — CNC cutting and press braking form the chamber body, liner and door frame to millimetre drawings.
- Welding & Forming — TIG and robot welding seal the chamber, followed by stress relief and surface treatment.
- Assembly & Wiring — Refrigeration, electrical cabinets, sensors and control panels are installed and wired to the schematic.
- Debugging & Calibration — Commissioning runs temperature, humidity, vibration and load profiles; data is logged per unit.
- Packing & Documents — Crating, manuals, certificates and the QC file are completed and sealed for dispatch.
- Delivery & Support — Shipment tracking, on-site installation and operator training are arranged with local partners.
Equipment referenced in this guide
- 150L Climate Test Chamber — Climate Test Chamber, manufactured in-house with per-unit calibration.
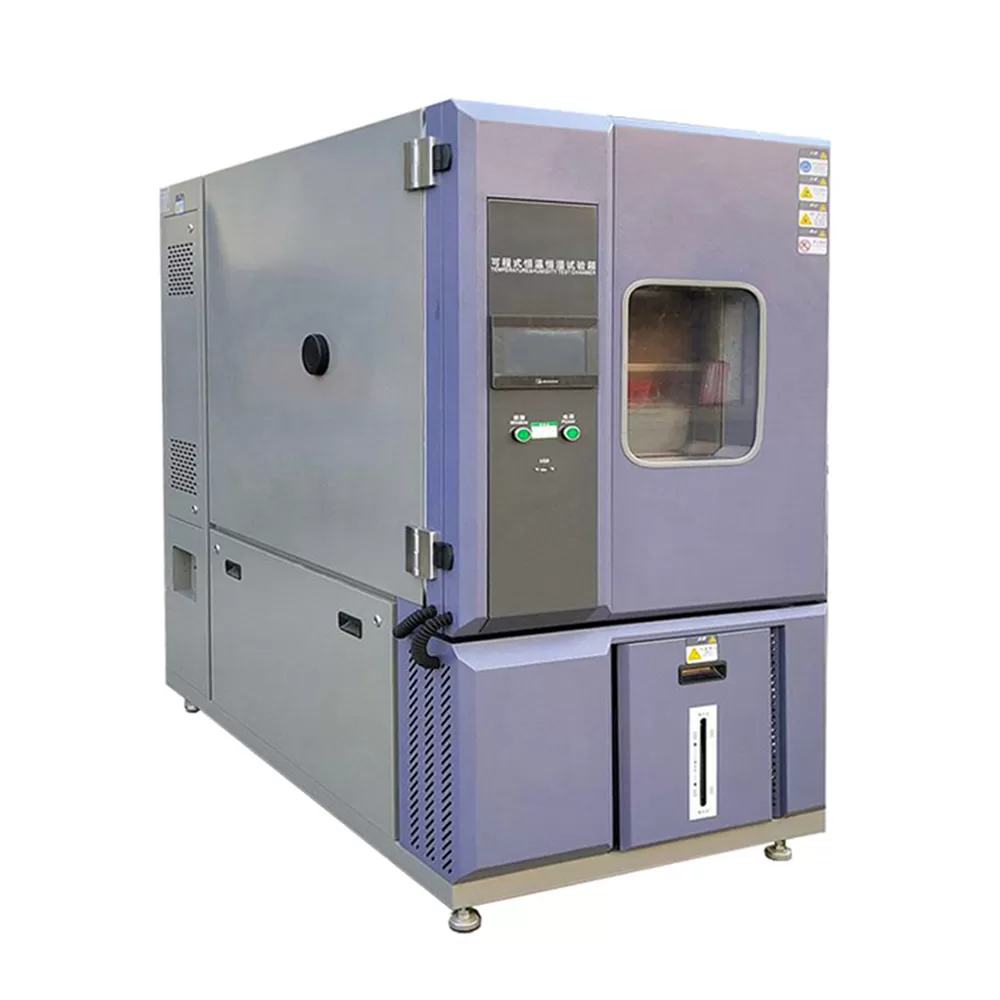
- 1000L Climate Test Chamber — Climate Test Chamber, manufactured in-house with per-unit calibration.
Conclusion
Specification is where a procurement process starts, but it is not where the result is decided. The variables that separate a repeatable test from an arguable one are the ones the manufacturer controls: the geometry of the chamber, the tightness of the weld, the stability of the control loop and the discipline of the calibration bench. Those are the variables worth asking about, because they are the ones that will still be there when the instrument is three years old and a colleague asks why the new machine and the old one give different numbers on the same specimen.
If you have a specification in front of you that has a profile, a volume and a tolerance, send it over. Our engineers will respond with a configuration, a lead time and the specific items in the manufacturing route that will affect your result.