Flammability Testing: Reading UL 94 and ISO 4589 Classifications
Polymer characterisation is a set of complementary methods, and the common mistake is to run one test and draw a broad conclusion from it. Each method answers a specific question about the material, and a laboratory that understands the questions can plan equipment accordingly.
Polymer characterisation is a set of complementary methods, and the common mistake is to run one test and draw a broad conclusion from it. Each method answers a specific question about the material, and a laboratory that understands the questions can plan equipment accordingly.
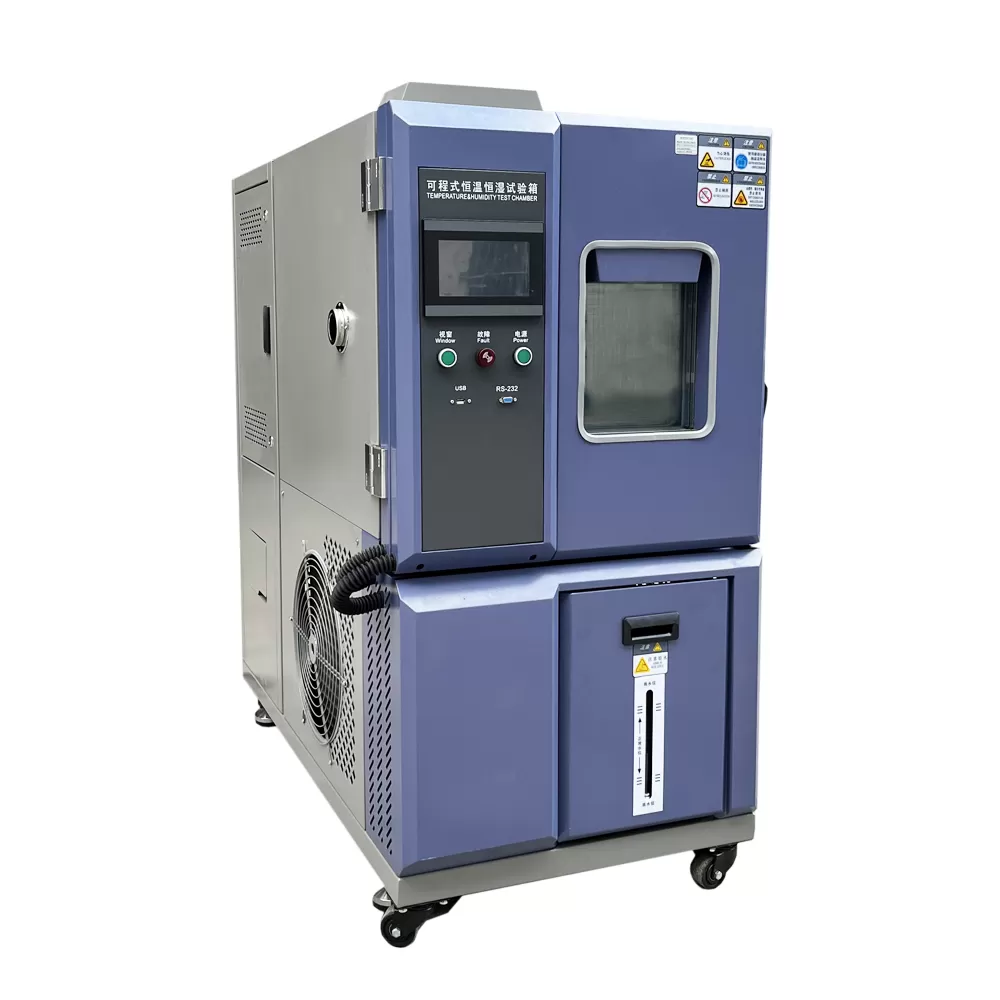
Applying that to a real purchase is easier when the equipment comes from a supplier that builds rather than assembles. 150L Climate Test Chamber is a typical example of a machine where the specification sheet is only half the story, because the fabrication and commissioning route determines how the numbers behave in service.
What to verify before you specify
1. MFR and VICAT answer different questions
Melt flow rate describes viscosity under a defined load and temperature. The Vicat softening temperature describes the temperature at which a defined indenter penetrates a specimen under a defined load. They are not substitutes, and both are needed for a full material description.
2. Heat conditioning governs the result
Both methods require the specimen to be conditioned at a defined temperature and humidity before testing. Skipping or shortening the conditioning step is a common source of scatter between laboratories.
3. Flammability rating depends on the specimen orientation
UL 94 ratings are assigned to a specific orientation and thickness. A 1.5 mm specimen rated V-0 does not transfer to a 3 mm specimen, and the flame-retardant compound in the material may behave differently at a different thickness.
4. Impact testing needs the right fixture geometry
Charpy and Izod specimens are not interchangeable, and the notch geometry is part of the standard. A worn or incorrectly machined notch changes the energy required to fracture.
5. Sample preparation often dominates the error budget
Moulding, conditioning and specimen machining contribute more variance than the instrument itself in most polymer labs.
6. Plan for the workflow around the instrument
Polymer testing involves heating, weighing, conditioning and machining. The bottleneck is usually the preparation area rather than the measurement device, and that is where the layout effort should go.
Mistakes that show up in the acceptance report
- Comparing Vicat temperature with melt flow rate as if they were equivalent.
- Testing impact specimens with a notch of the wrong radius or angle.
- Assigning a UL 94 rating to a thickness that was not tested.
- Under-investing in specimen preparation equipment and blaming the instrument.
Manufacturing capability as a risk-reduction strategy
When a qualification programme has a fixed window, the biggest risk is not the test failing. It is a delivery date moving.
Engineering drawings, chamber fabrication, control cabinet wiring and commissioning all sit under one roof, so a specification change during the project is absorbed by the factory rather than passed between suppliers.
Owning the production route means the critical path is the one we control. Non-standard chamber sizes, unusual instrumentation and special test profiles do not become a procurement problem.
The quality file travels with the machine. IQC at material intake, IPQC during assembly and OQC before crating mean the acceptance decision at your laboratory is traceable to our production floor.
- In-house Manufacturing: Every machine is engineered, welded, assembled and tested under one roof. Two production plants control tolerances from raw sheet steel to final calibration.
- OEM & ODM Engineering: Drawings, PLC logic, instrumentation and chamber geometry are developed in-house, so non-standard chamber sizes and test profiles ship without external dependencies.
- Full In-House Calibration: Temperature, humidity, pressure and load cells are calibrated on our own accredited benches before shipment, with certificates issued per unit.
- QC at Every Stage: IQC, IPQC and OQC gates sit between material intake, welding, assembly and dispatch. Nothing leaves the line without a signed inspection record.
How the equipment is produced
The production route below is the one every HAOEN machine follows. It is listed because the steps a manufacturer controls are the steps that determine whether your laboratory receives a machine that performs as specified on the day it is commissioned, and still performs two years later.
- Engineering Drawing — Chamber geometry, load frame, airflow and instrumentation are modelled and reviewed before any steel is cut.
- Material Intake — Sheet metal, compressors, sensors and electrical parts pass incoming inspection against incoming QC checkpoints.
- Cutting & Bending — CNC cutting and press braking form the chamber body, liner and door frame to millimetre drawings.
- Welding & Forming — TIG and robot welding seal the chamber, followed by stress relief and surface treatment.
- Assembly & Wiring — Refrigeration, electrical cabinets, sensors and control panels are installed and wired to the schematic.
- Debugging & Calibration — Commissioning runs temperature, humidity, vibration and load profiles; data is logged per unit.
- Packing & Documents — Crating, manuals, certificates and the QC file are completed and sealed for dispatch.
- Delivery & Support — Shipment tracking, on-site installation and operator training are arranged with local partners.
Equipment referenced in this guide
- 150L Climate Test Chamber — Climate Test Chamber, manufactured in-house with per-unit calibration.
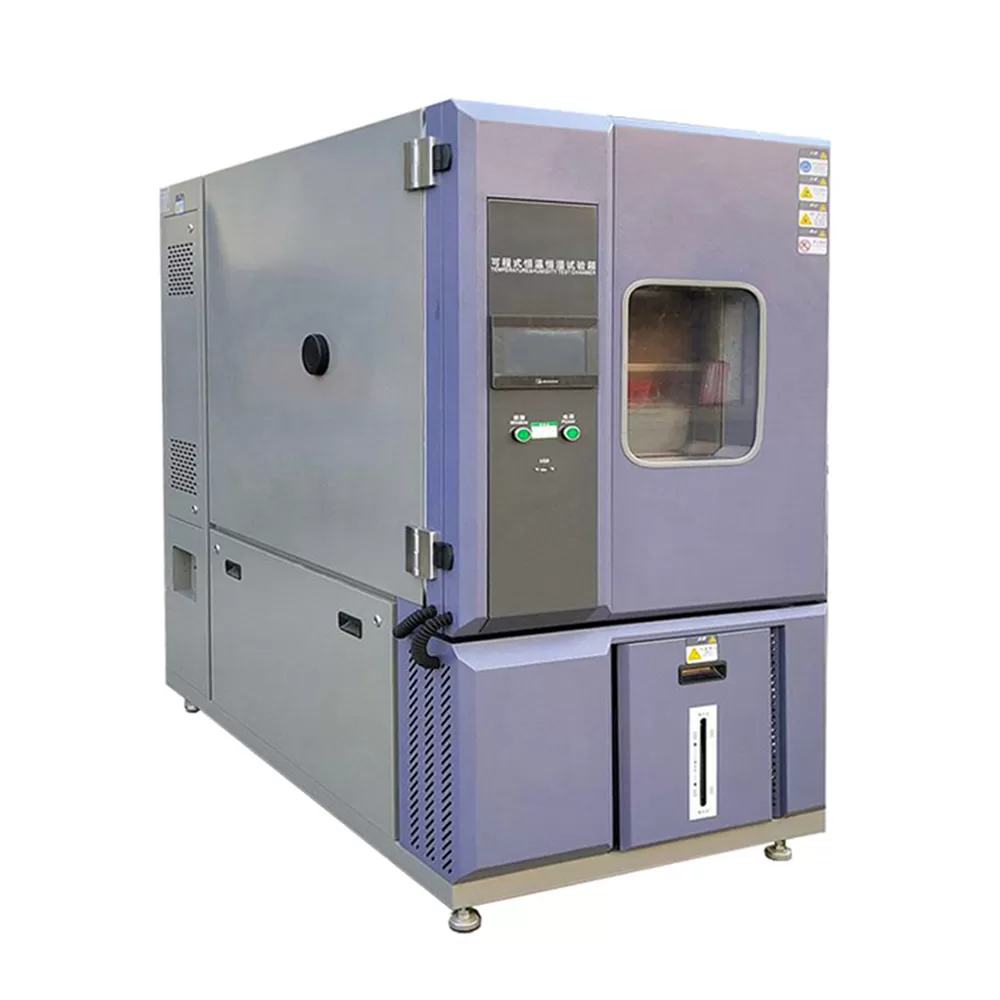
- 1000L Climate Test Chamber — Climate Test Chamber, manufactured in-house with per-unit calibration.
Conclusion
Specification is where a procurement process starts, but it is not where the result is decided. The variables that separate a repeatable test from an arguable one are the ones the manufacturer controls: the geometry of the chamber, the tightness of the weld, the stability of the control loop and the discipline of the calibration bench. Those are the variables worth asking about, because they are the ones that will still be there when the instrument is three years old and a colleague asks why the new machine and the old one give different numbers on the same specimen.
If you have a specification in front of you that has a profile, a volume and a tolerance, send it over. Our engineers will respond with a configuration, a lead time and the specific items in the manufacturing route that will affect your result.