From Specification to Production: How Custom Test Equipment Actually Gets Built
Custom equipment is a relationship, not a purchase order. The laboratories that get the best result from a non-standard machine are the ones that engage the manufacturer early enough to influence the design rather than late enough to request a change.
Custom equipment is a relationship, not a purchase order. The laboratories that get the best result from a non-standard machine are the ones that engage the manufacturer early enough to influence the design rather than late enough to request a change.
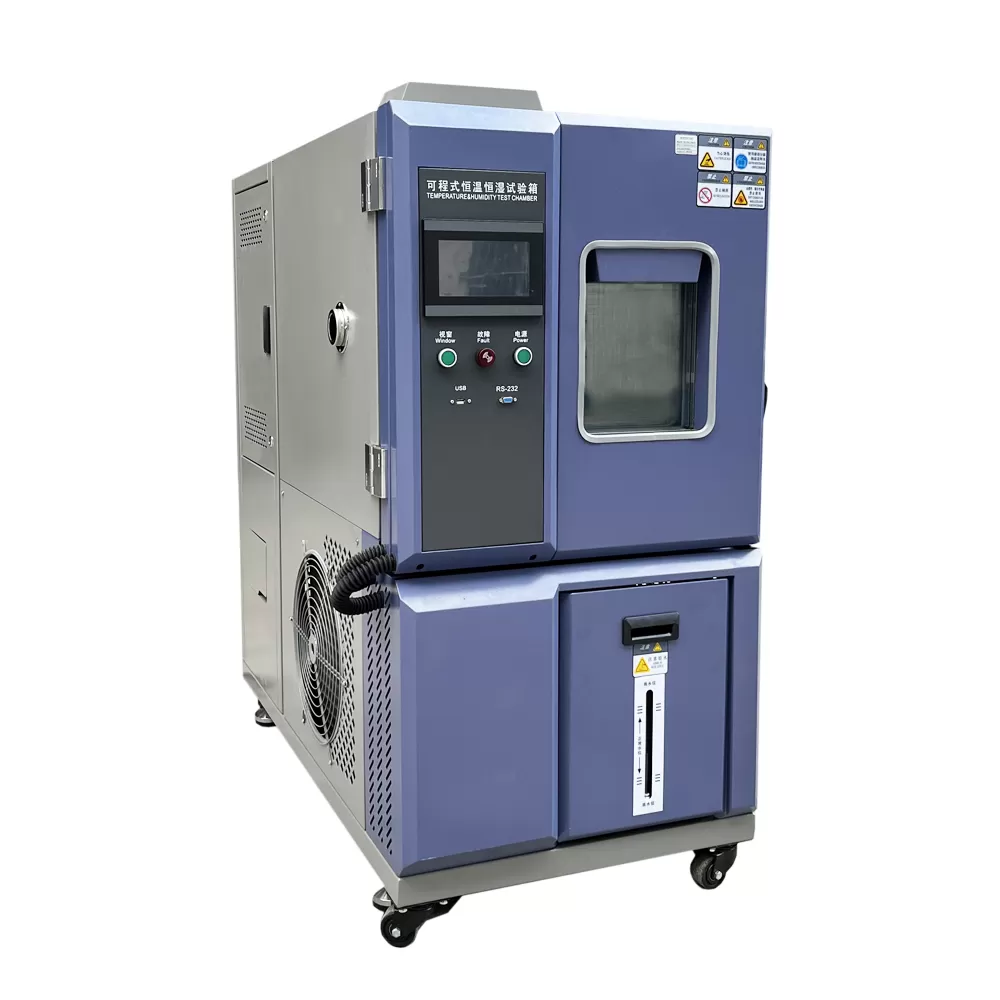
Applying that to a real purchase is easier when the equipment comes from a supplier that builds rather than assembles. 150L Climate Test Chamber is a typical example of a machine where the specification sheet is only half the story, because the fabrication and commissioning route determines how the numbers behave in service.
What to verify before you specify
1. Define the constraint, not the wish list
A manufacturer can usually work with a stated limitation — a footprint, a temperature range, an interface — more effectively than with an open request to modify the machine. Constraints produce buildable designs.
2. Engage before the drawing is frozen
Changes made during the design stage are cheap. Changes made after fabrication has started are expensive, and the manufacturer has to carry the risk of a re-validated chamber.
3. Expect the interface to need attention
Customisation frequently creates a mismatch at the boundary between the machine and the existing laboratory, whether that is power, cooling water, data output or the door swing in a confined room.
4. Documentation follows the build
A custom machine still needs the standard document set, and the person who writes it should have been involved in the build. Documentation written afterwards from a specification is where omissions appear.
5. Define the acceptance criteria up front
What will be measured, against which reference, with what tolerance, and by whom. A custom machine without a written acceptance procedure generates endless discussion after delivery.
6. Plan the maintenance route early
A machine with non-standard parts needs a service plan that the manufacturer can honour years later. This is easier to arrange while the design is still being developed.
Mistakes that show up in the acceptance report
- Sending a fully drawn machine and expecting a quotation to be the only conversation.
- Requesting changes after fabrication has started.
- Forgetting the laboratory interface in the specification.
- Accepting delivery without a written acceptance procedure and measured results.
The cost of a machine that arrives and has to be corrected
Most delays attributed to supply chains are actually attributable to a mismatch that was cheap to fix and expensive to fix late.
A chamber that is specified around a footprint, a temperature range and an interface produces a buildable design. An open-ended modification request produces a negotiation that consumes weeks.
Owning the production route means a non-standard chamber size or an unusual instrumentation requirement is a scheduling question on our floor rather than a procurement cycle.
Per-unit calibration performed before packing means the acceptance discussion at the laboratory is about using the machine, not about establishing whether it ever worked.
- In-house Manufacturing: Every machine is engineered, welded, assembled and tested under one roof. Two production plants control tolerances from raw sheet steel to final calibration.
- OEM & ODM Engineering: Drawings, PLC logic, instrumentation and chamber geometry are developed in-house, so non-standard chamber sizes and test profiles ship without external dependencies.
- Full In-House Calibration: Temperature, humidity, pressure and load cells are calibrated on our own accredited benches before shipment, with certificates issued per unit.
- QC at Every Stage: IQC, IPQC and OQC gates sit between material intake, welding, assembly and dispatch. Nothing leaves the line without a signed inspection record.
How the equipment is produced
The production route below is the one every HAOEN machine follows. It is listed because the steps a manufacturer controls are the steps that determine whether your laboratory receives a machine that performs as specified on the day it is commissioned, and still performs two years later.
- Engineering Drawing — Chamber geometry, load frame, airflow and instrumentation are modelled and reviewed before any steel is cut.
- Material Intake — Sheet metal, compressors, sensors and electrical parts pass incoming inspection against incoming QC checkpoints.
- Cutting & Bending — CNC cutting and press braking form the chamber body, liner and door frame to millimetre drawings.
- Welding & Forming — TIG and robot welding seal the chamber, followed by stress relief and surface treatment.
- Assembly & Wiring — Refrigeration, electrical cabinets, sensors and control panels are installed and wired to the schematic.
- Debugging & Calibration — Commissioning runs temperature, humidity, vibration and load profiles; data is logged per unit.
- Packing & Documents — Crating, manuals, certificates and the QC file are completed and sealed for dispatch.
- Delivery & Support — Shipment tracking, on-site installation and operator training are arranged with local partners.
Equipment referenced in this guide
- 150L Climate Test Chamber — Climate Test Chamber, manufactured in-house with per-unit calibration.
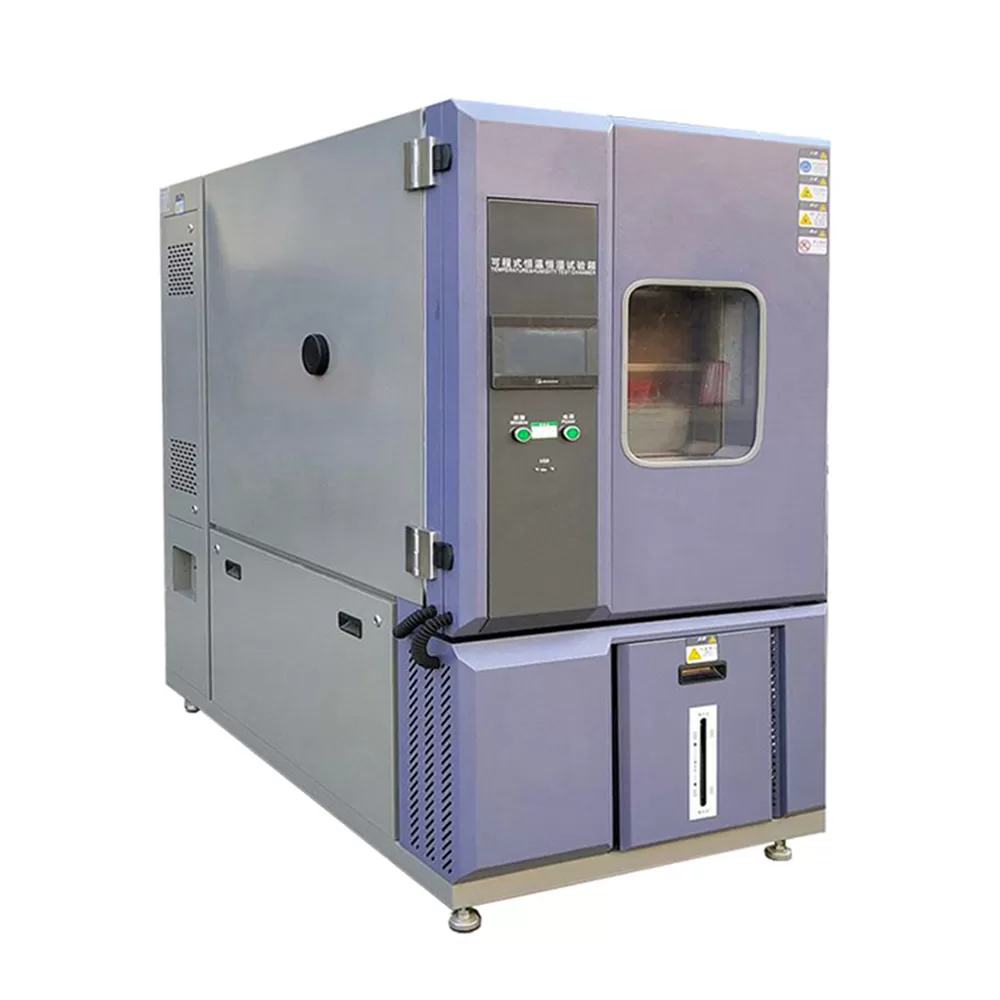
- 1000L Climate Test Chamber — Climate Test Chamber, manufactured in-house with per-unit calibration.
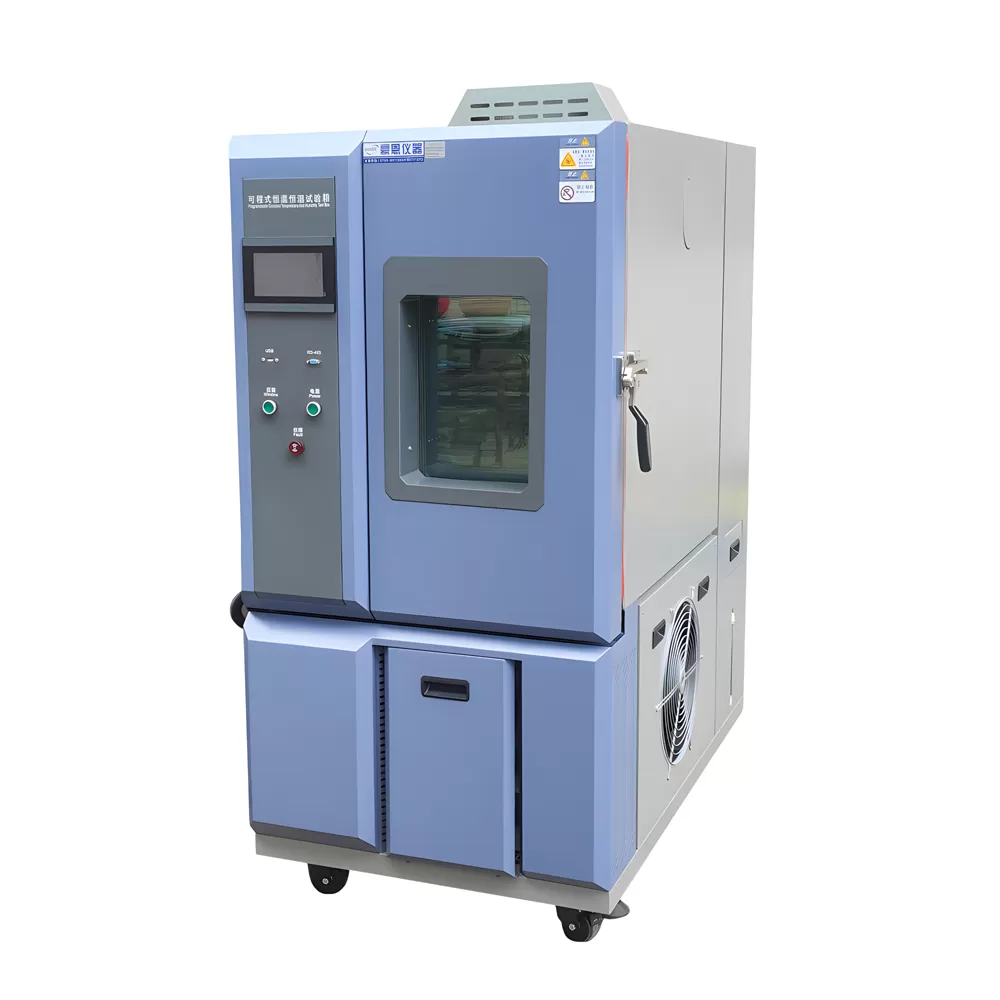
- 225L Climate Test Chamber — Climate Test Chamber, manufactured in-house with per-unit calibration.
Conclusion
Specification is where a procurement process starts, but it is not where the result is decided. The variables that separate a repeatable test from an arguable one are the ones the manufacturer controls: the geometry of the chamber, the tightness of the weld, the stability of the control loop and the discipline of the calibration bench. Those are the variables worth asking about, because they are the ones that will still be there when the instrument is three years old and a colleague asks why the new machine and the old one give different numbers on the same specimen.
If you have a specification in front of you that has a profile, a volume and a tolerance, send it over. Our engineers will respond with a configuration, a lead time and the specific items in the manufacturing route that will affect your result.